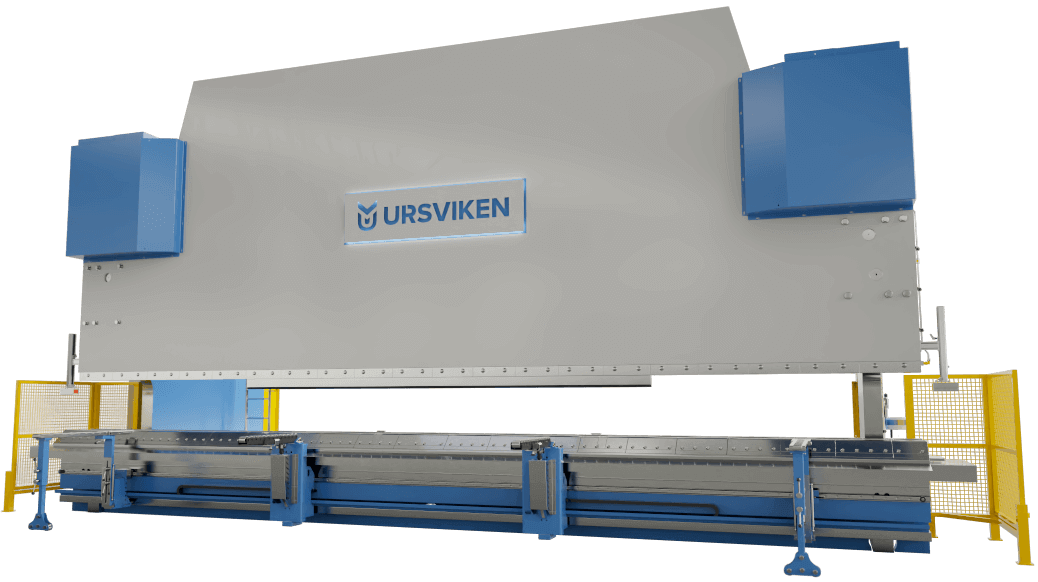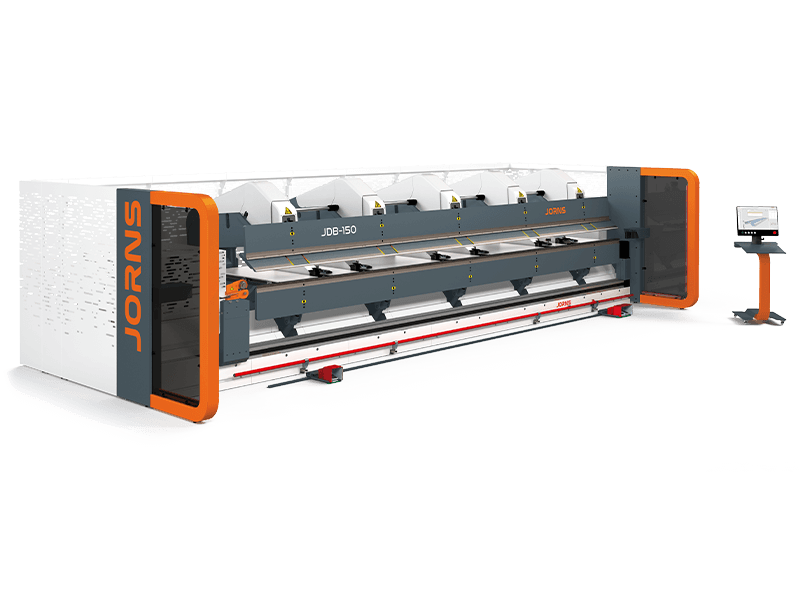
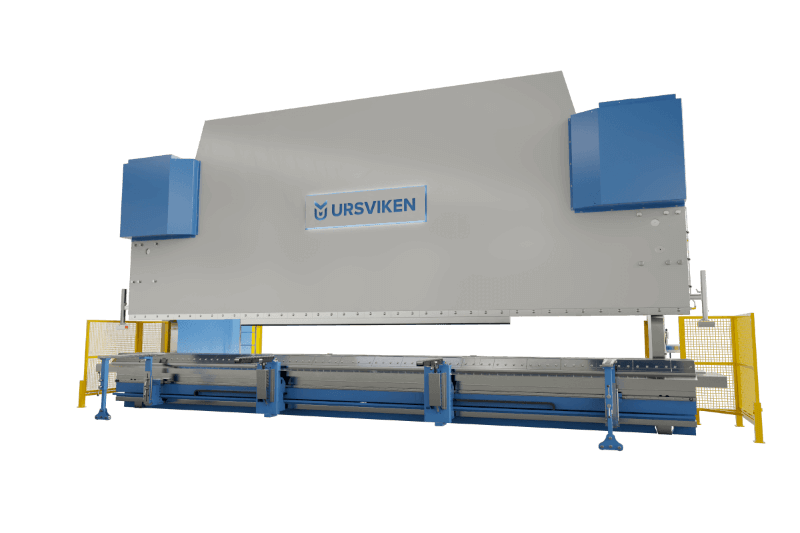
A press brake is an investment for fifteen years or longer. If you cut the tonnage or bend length too close, you will run into limits for years to come. If you buy more machine than you need, you tie up capital that sits idle. Here are the choices that matter most, with the rules of thumb behind them.
Tonnage: how much force do you need?
The required bending force depends on sheet thickness, the tensile strength of the material, the V-die opening chosen for the die, and the bend length.
Always calculate using your thickest and longest workpiece, and keep a margin. A machine that constantly runs at one hundred percent of its capacity wears out faster and leaves no room for heavier work in the future.
V-die opening and inside radius
A larger V-die opening requires less force and reduces the risk of cracking, but it also produces a larger inside radius (roughly the V-die opening divided by six) and a longer minimum flange. Narrow, closed profiles, on the other hand, require a small V-die opening and therefore more tonnage. Map out which profiles you produce most often before choosing a machine.
Bend length and deflection
Choose the bend length based on your largest workpiece, with some margin for tooling changes. Pay attention to deflection: the longer the press beam, the more it deflects in the centre under pressure. Without compensation, the centre of a long sheet ends up with a different angle than the ends. Hydraulic or CNC-controlled crowning corrects this. With long sheets and tight angular tolerances, this is not a luxury but a requirement.
Start from the workpiece, not from the machine.
Control: manual, NC or full CNC
- Manual or NC with one or two axes. Fine for simple bends in small batches. Requires more skill from the operator and more changeover time.
- Full CNC with a multi-axis back gauge (X, R, Z and sometimes additional axes) and angle measurement. Worthwhile as soon as you produce complex parts, change over often, or work in varying batch sizes. The control calculates the bend sequence and gauge positions and compensates for springback. Offline programming keeps the machine productive while you prepare the next job.
Ram drive
Hydraulic drives are robust and deliver a lot of force for the price. Servo-electric drives are faster, quieter, more accurate in repeatability and more energy-efficient, but the purchase price is higher and the maximum tonnage is more limited. Hybrid systems fall between the two. At high production volumes, the speed and lower energy consumption of electric drives quickly tip the balance.
Tooling and safety
Quick-clamping systems for upper and lower tooling save time at every changeover. Segmented tooling makes it possible to form boxes and short channels. Laser or camera guarding is now the standard; check that the system complies with the current Machinery Directive.
In summary
Start from the workpiece. Determine your thickest and longest sheet, your most common profiles and your batch sizes. Tonnage, bend length, control level and drive follow almost naturally from that. If you are unsure about the calculation, submit your typical workpieces to a specialist and have trial bends made with your own material.
Written by Triple AAA Machines
Ask for advice